What is kerf width?
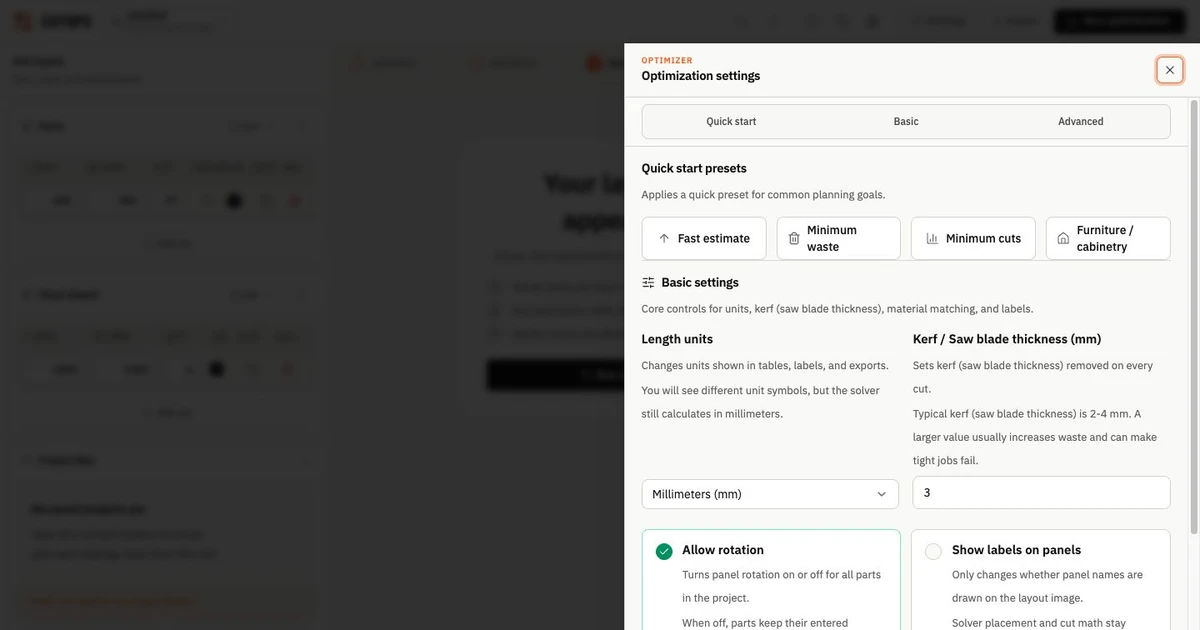
Kerf is the width of material removed by the cutting tool. In a rectangular cut list, the finished part dimensions and the space consumed by the cut are separate inputs. A layout can have enough total material area and still fail to fit once the cutting width is included.
Use this guide to measure kerf, calculate a simple row allowance, and check the effect in a complete panel layout. For a ready-to-run project, open the 3 mm kerf example in CutOps.
Measure the cut, not just the blade body
The blade body thickness is not always the width of the finished cut. Use the installed tool and the material you intend to cut. Start with the manufacturer's cutting-width specification, then verify it with a controlled test cut when practical.
For a straight cut through a test piece:
- Measure the piece width before cutting.
- Make one cut that divides it into two retained pieces.
- Measure both remaining widths in the same direction.
- Subtract their sum from the original width.
The difference is an estimate of the material removed by that cut. Measurement precision, tool condition, and the cutting process affect the result. Repeat the check if the result is inconsistent, and follow your workshop's measurement procedure for the required tolerance.
Record the tool, material, unit, and measured value with the job. Recheck after a blade change or a process adjustment instead of carrying an old assumption into the next layout.
A simple kerf allowance formula
For a straight row of finished parts, with one separating cut between each adjacent pair:
Minimum row span = sum of finished part widths + (number of parts - 1) x kerf
This formula counts the internal separating cuts. It does not include edge trim, a cut separating the row from a remaining offcut, or other cuts needed to make the full two-dimensional layout. Add those allowances where the actual cutting method requires them.
Worked example: two 600 mm parts and 3 mm kerf
The CutOps kerf example uses a 2440 x 1220 mm stock sheet and 3 mm kerf. Consider two of its 600 mm-wide parts side by side across the 1220 mm dimension:
- Finished part widths: 600 + 600 = 1200 mm.
- One internal separating cut: 3 mm.
- Minimum row span: 600 + 3 + 600 = 1203 mm.
- Width remaining before any additional allowance: 1220 - 1203 = 17 mm.
Ignoring kerf would suggest 20 mm remains. That 3 mm difference is the allowance for one separating cut, not a waste percentage or a guarantee that the complete job fits.
A row calculation checks one dimension. The complete layout also has to place the other parts, respect their orientation, fit the available stock, and account for its cutting geometry. Inspect the calculated result rather than using total part area as proof of feasibility.
A tight strip shows why the gap matters
In a separate checked CutOps run, a 1200 x 400 mm stock strip was given two 600 x 400 mm parts with rotation disabled. With 0 mm kerf, both parts fit. With 3 mm kerf, only one part fit and the second remained unplaced: the two finished widths plus their separating cut require 1203 mm.
That comparison changes only kerf. It illustrates a fit constraint, rather than predicting the number of sheets or waste for a larger job.
Try the complete example
The kerf example loads:
- One 2440 x 1220 mm stock sheet.
- Six 600 x 400 mm parts.
- Two 1000 x 300 mm parts.
- A 3 mm kerf setting.
The checked example places all eight parts on one sheet at 68.5% utilization. The figure is the part area divided by the used stock area; it is not an estimate of savings compared with your current process.
The example is free and does not require an account. It gives you stock, part rows, and a calculated layout to review together. If a project is already open, confirm replacement before loading the sample.
Review the placed dimensions, used sheet count, and any unplaced parts. Change kerf to the measured value for your own tool, run optimization again, and compare what changed. The demonstration setting is not a recommendation for every blade or material.
Enter kerf once in CutOps
Keep the requested finished sizes in the parts table. Set the cutting width separately in the optimizer settings, using the project's unit.
Do not subtract kerf from the part sizes to make the layout fit. That changes the finished components you are asking for. Do not add kerf to every part yourself either: CutOps already reserves space for the cut in its placement geometry, so doing both can count the allowance twice.
After changing kerf:
- Check stock dimensions and available quantities.
- Keep any required per-part rotation locks.
- Run optimization again.
- Inspect the layout and unplaced parts.
- Export the result from that same run.
Keep kerf and per-part rotation locks consistent with the job. CutOps supports material and grain enforcement, strategy comparison, and advanced controls. When using strategy comparison, keep the same kerf assumption across the alternatives you compare.
Kerf, edge trim, and tolerance are different
Kerf describes the material consumed by a cut. Edge trim describes stock you remove or exclude to obtain a usable boundary. Tolerance describes the acceptable variation in the finished part.
Do not combine all three into an inflated kerf value. That can reserve extra space between every part while still failing to represent the intended edge requirement. Define the usable stock dimensions and cutting assumptions explicitly, then verify that the finished dimensions meet the job specification.
CutOps plans rectangles and does not measure your machine or validate physical tolerances. The workshop still needs to check the actual cutting method, material condition, and required finishing allowances.
Common setup mistakes
Mixing units
A value entered in millimetres has a different meaning from the same number entered in inches. Confirm the project unit and the displayed kerf value before running or rerunning a saved project.
Using one value for every cutting process
A saw, router, laser, and glass scoring process can require different separation assumptions. Use the value appropriate to the tool and material; the 3 mm example illustrates a saw allowance and is not a universal default.
Changing the blade after the plan is approved
A new tool can change the effective cut width. Update kerf and rerun active jobs before exporting a replacement plan.
Checking utilization but ignoring unplaced parts
A high utilization figure does not mean every requested part was placed. Check remaining quantities and dimensions alongside the layout, particularly when stock is limited.
Before handing off the plan
Confirm the finished part sizes, stock quantities, unit, kerf value, rotation requirements, and any unplaced parts. Keep the measured tool setting and required finishing allowances with the workshop's job records. Export only after reviewing the result calculated with those inputs.
Use the kerf cutting optimizer to apply these checks to a job, or continue with grain direction in panel cutting when orientation restricts the layout.